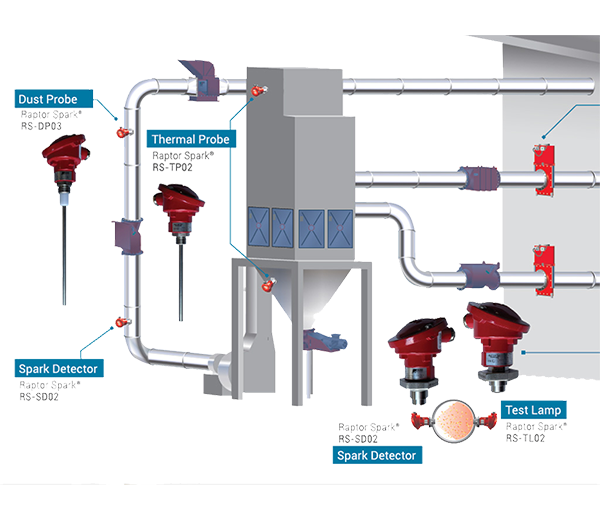
The Raptor Spark® Detection and Extinguishing System is an FM Approved safety device that is designed to detect and extinguish sparks and glowing embers that are traveling through a duct system.
The Raptor Spark® Detection and Extinguishing System is an FM Approved safety device that is designed to detect and extinguish sparks and glowing embers that are traveling through a duct system.
The hazard is detected by infrared sensors and extinguished with water spray nozzles within milliseconds of detection. The Raptor Spark® detection control unit has the capacity to receive hazard alert signals from multiple components and monitor multiple duct-zones and vessels.
The Raptor Spark® Detection and Extinguishing System is an essential Fire Protection, Fire Isolation and Diversion device that is commonly installed with Raptor Gate™ High Speed Abort Gates, FireBreak Shutters, Vigilex Explosion Vents and explosion certified VDL Rotary Valves. Typical automatic functions include hazard detection, system shut-down, isolation/abort, and extinguish and/or suppression.
A spark detection and extinguishing system (like our Raptor line) continuously monitors ductwork for sparks or embers generated upstream by grinding, cutting, or other hot processes, and automatically extinguishes them with a water mist before they reach a filter or collector where they could ignite accumulated dust. It's typically recommended wherever a process both generates sparks and feeds a dry dust collection system.
An explosion vent (like our Vigilex domed or flameless vent panels) is designed to relieve pressure safely to the outside of a vessel if a dust explosion occurs inside it. An explosion isolation valve (like our Vigiflap valves) is designed to stop flame and pressure from traveling through ductwork from one piece of equipment to another, preventing a secondary explosion elsewhere in the system. Most combustible-dust systems use both as part of a layered protection strategy.
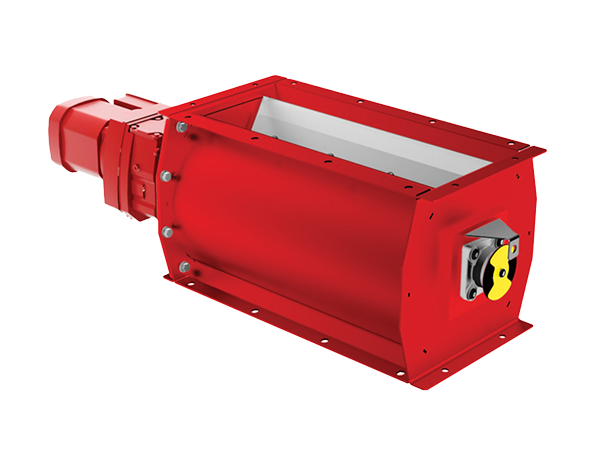
Sledge Tech is a proud supplier of Boss Process Rotary Valves. The Boss Process BS Series…
Learn More →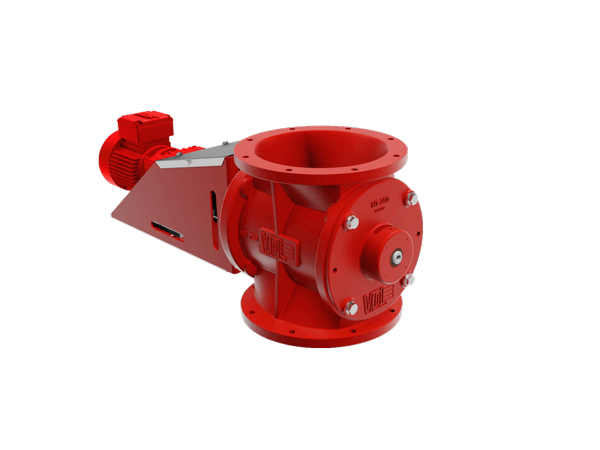
Sledge Tech is a proud supplier of Boss Process Rotary Valves. The Boss Process HT Series…
Learn More →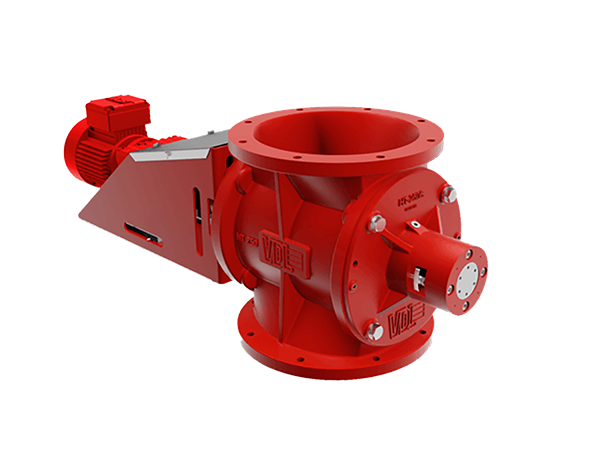
Sledge Tech is a proud supplier of Boss Process Rotary Valves. The Boss Process HTS Series…
Learn More →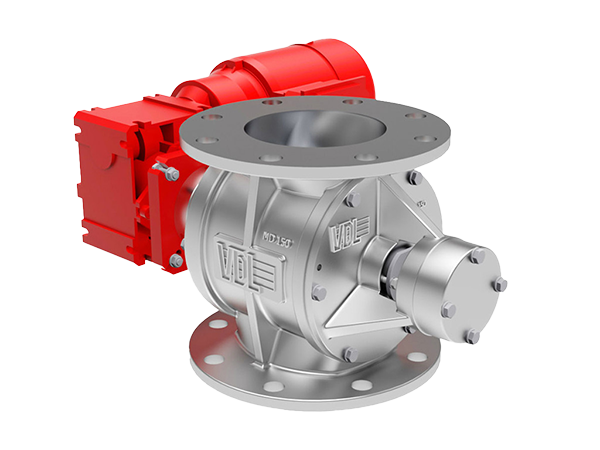
Sledge Tech is a proud supplier of Boss Process Rotary Valves. The Boss Process MD Series…
Learn More →Get a free consultation with a Sledge Tech filtration engineer — most quotes turned around in 24 hours.